
201 589 00 51 00
Spot weld cutter
Commercially available tools
Number | Designation | |
WH58.30-Z-1002-01A | Ball cutter, dia. 12 mm | |
WH58.30-Z-1006-01A | Vario Drill WS 91 spot weld removing tool | |
WH58.30-Z-1001-03A | Round wire brush, braided, dia. 70 mm | |
WH58.30-Z-1021-04A | Cutting disk, dia. 65 mm, 80 m/s (max. 23,500 rpm) | |
WH58.30-Z-1024-04A | Abrasive disk, dia. 115 mm, 80 m/s (max. 13,250 rpm) |
Workshop equipment
WE58.40-Z-1001-03A | Drill (electric/pneumatic) |
WE58.40-Z-1002-03A | Straight grinder (electric/pneumatic) |
WE58.40-Z-1003-03A | Angle grinder (electric/pneumatic) |
WE58.40-Z-1004-03A | Body saw (electric/pneumatic) |
P63.50-0501-06
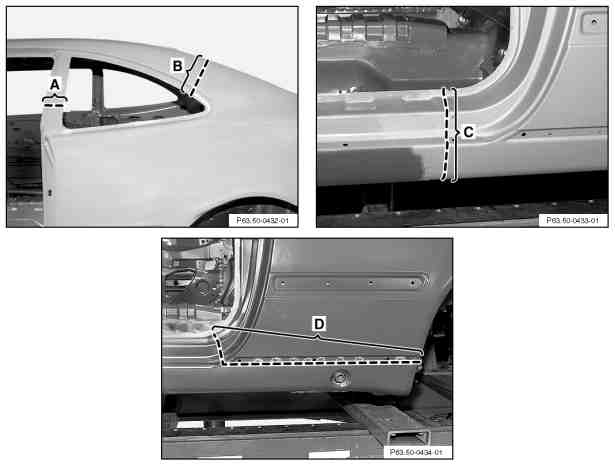
1 Mark rear fender in areas A-C (dotted lines), and cut with body saw.
Do not damage inner sections of B and C-pillars beneath.
Perform repair according to scope of damage between separating cut C and D.
The fuel tank can remain in the vehicle for separating cut D.

P63.50-0502-09
2 Expose welded areas.
3 Cut out spot welds in areas A - G.

P63.50-0503-06
4 Cut out spot welds in area A .
Expose brazed seams in areas B and C and disconnect.
Separate weld in area D.
5 Heat up B and C-pillars in shaded area with hot air gun (foam filled area).
6 Remove deformed rear fender.

P63.50-0504-09
7 Grind down spot weld residues.
8 Then grind connection surfaces down to bare metal in shaded areas.
9 Grind spot welding flanges down to bare metal on both sides.
10 Coat insides of spot welding flanges with zinc dust paint.