Additional information can be found in the superordinate service document.
The safety information in the superordinate service document must be observed.
The following operation steps are shown on model 910.631 with code T16 (Sliding door, right) on the right side of the vehicle and must be similarly performed on vehicles with code T19 (Sliding door, left) in the case of damage to the left side of the vehicle.

1 | Mark separating points on B-pillar outer section (1) (areas A and B). |
Do not undershoot dimensions (a, b) under any circumstances. |
Mark separating points (areas A and B) according to the degree of damage. |
Observe dimensions (A, B). |
2 | Separate B-pillar outer section (1) at the separating points (areas A and B). |
Do not make the cuts too deep. |
Commercially available devices/tools |
a | Dimension ( 200 mm) |
b | Dimension ( 40 mm) |
D63.20-1506-06

3 | Expose spot welds on B-pillar outer section (1) (areas C, D, E, E1, F, G and H). |
Commercially available devices/tools |
4 | Mill off spot welds on B-pillar outer section (1) (areas C, D, E, E1, F, G and H). |
Mill off spot welds through two panel thicknesses (areas G and H). |
Commercially available devices/tools |
5 | Heat B-pillar outer section (1) in crosshatched areas (areas I and J). |
6 | Remove damaged B-pillar outer section (1). |
D63.20-1507-06
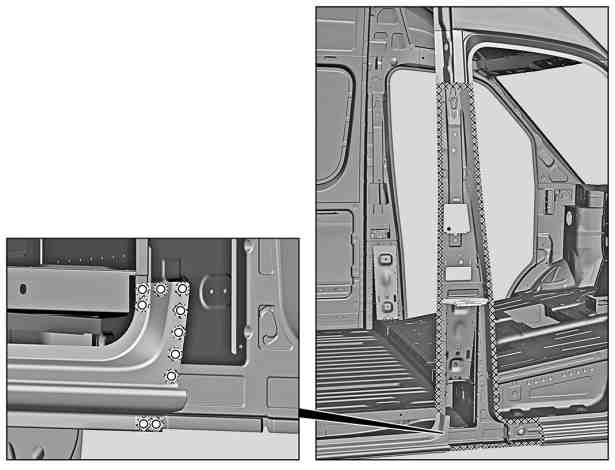
7 | Grind mating surfaces down to bare metal in cross-hatched areas and around holes. |
Sand down spot weld flanges to bare metal on both sides. |
Commercially available devices/tools |
8 | Remove shavings and milling chips. |
Commercially available devices/tools |
9 | Zinc dust paint to insides of spot weld flanges. |
D63.20-1508-06