00-0901 Repairing threaded holes with heli-coil inserts
Data | ||
Metric thread | Core plug hole | Outer of twist drill |
M6 | 6.31 6.04 | 6.1-6.2-6.25 |
M8 | 8.35 8.04 | 8.1-8.2-8.25-8.3 |
M81 | 8.32 8.04 | 8.1-8.2-8.25-8.3 |
M10 | 10.40 10.05 | 10.25 |
M12 | 12.50 12.05 | 12.25-12.5 |
M121.5 | 12.43 12.05 | 12.25 |
M14 | 14.53 14.06 | 14.25-14.5 |
M141.5 | 14.43 14.05 | 14.25 |
M152 | 15.30 15.20 | 15.25 |
M16 | 16.53 16.06 | 16.25-16.5 |
M161.5 | 16.43 16.05 | 16.25 |
M241.5 | 24.43 24.05 | 24.25 |
M261.5 | 26.43 26.05 | 26.25 |
M301.5 | 30.43 30.05 | 30.25 |


Special tools
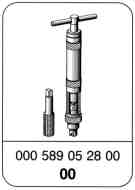
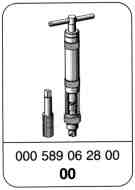
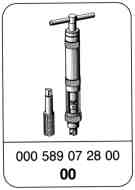
Repairing
1 Widen plug hole with twist drill.
Note
Do not counter-sink hole.
2 Re-tap the damaged thread with the special heli-coil thread tap.

3 Fit a spindle (1) and mouthpiece (2) matching the size of thread to the installation tool.
Note
The slot on the mouthpiece (2) must be aligned with the marking on the installation tool (arrows).

4 Place heli-coil threaded insert (3) into the spindle (1) in the installation tool.
Note
The driver stud of the heli-coil thread insert must be positioned in the slot (arrow).

5 Turn threaded insert (3) with the spindle through the mouthpiece until the insert is flush at the front.

6 Position installation tool on the threaded hole and turn in the insert without exerting any pressure on the spindle.
Note
Turn in insert 1/2 to 1 1/2 turns deeper than the surface of the tapped hole.
7 Remove driver stud up to M12 with the stud snap. For threaded inserts greater than M12 remove driver stud by moving up and down with pointed pliers.