

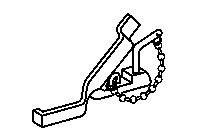
201 589 00 51 00
210 589 09 23 00
210 589 10 23 00
Spot weld cutter
Template for right rear fender at front bottom
Template for left rear fender at front bottom
Commercially available tools
Number | Designation | |
WH58.30-Z-1002-01A | Ball cutter, dia. 12 mm | |
WH58.30-Z-1006-01A | Vario Drill WS 91 spot weld removing tool | |
WH58.30-Z-1001-03A | Round wire brush, braided, dia. 70 mm | |
WH58.30-Z-1021-04A | Cutting disk, dia. 65 mm, 80 m/s (max. 23,500 rpm) | |
WH58.30-Z-1024-04A | Abrasive disk, dia. 115 mm, 80 m/s (max. 13,250 rpm) | |
WH58.30-Z-1001-40A | Tarp (fire-resistant) |
Workshop equipment
WE58.40-Z-1001-03A | Drill (electric/pneumatic) |
WE58.40-Z-1002-03A | Straight grinder (electric/pneumatic) |
WE58.40-Z-1003-03A | Angle grinder (electric/pneumatic) |
WE58.40-Z-1004-03A | Body saw (electric/pneumatic) |

P63.50-0364-09
1 Mark separation point on rocker panel with aid of template and cut with body saw at C and D-pillars to fit new part (dotted lines).
Do not damage C and D-pillars beneath.

P63.50-0367-09
2 Expose spot welds and brazed seams, cut out or separate (areas A-K and arrow).
3 Heat C-pillar in shaded area with hot air gun.
C-pillar is filled with foam.
4 Remove deformed rear fender.


P63.50-0375-01
P63.50-0374-01

P63.50-0376-09
5 Grind connection surfaces for installation of new part down to bare metal (shaded areas and arrows).
6 Grind both sides of spot welding flanges down to bare metal.
7 Coat insides of spot welding flanges with zinc dust paint.