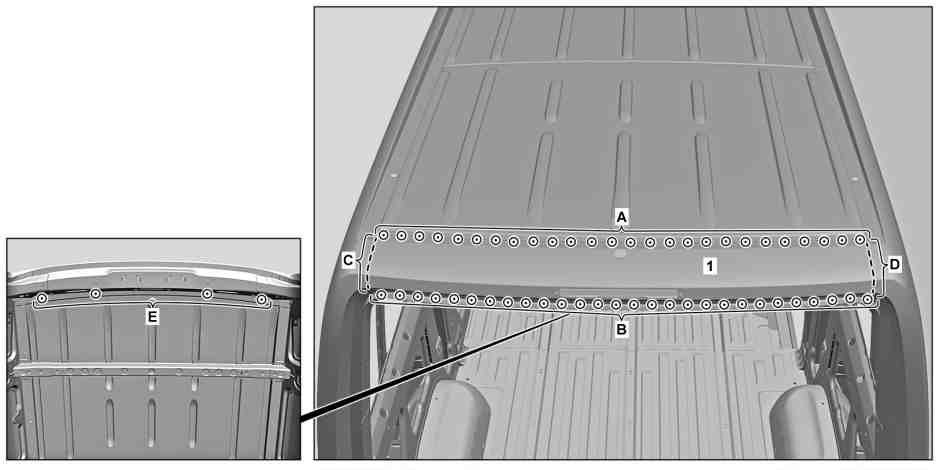
The following operation steps are shown on model 907.733 with code D03 (Roof and rear-end doors, high version).
D65.10-1359-09
1
Mark separation lines on roof paneling rear section (1) (areas C and D).
Scribe separation lines on edges (areas C and D).
2
Cut rear section of roof paneling (1) at separating points (areas C and D).
3
Expose spot welds on roof paneling rear section (1) (areas A, B, and E).
4
Mill off spot welds on rear section of roof paneling (1) (areas A, B and E).
Model 907.6/7 except code D05 (Super-high roof) except code D06 (Super-high roof painted in vehicle colour) Model 910.6 Cut out spot welds through two sheet metal thicknesses (areas A and E).
Model 907.6/7 with code D05 (Super-high roof) Model 907.6/7 with code D06 (Super-high roof painted in vehicle colour) Cut out spot welds through one sheet metal thickness (areas A and E).
5
Remove damaged rear section of roof paneling (1).
D65.10-1361-09
6
Sand down mating surfaces to bare metal in cross-hatched areas .
Sand down spot weld flanges to bare metal on both sides.
7
Grind areas around holes down to bare metal.
8
Remove shavings and milling chips.
9
Apply zinc dust paint to insides of spot weld flanges.
Powiązane dokumenty
as0000z001701a Niebezpieczeństwo obrażeńo elementy pojazdu o ostrych krawędziach.