Additional information can be found in the superordinate service document.
The safety information in the superordinate service document must be observed.
The next steps are shown on the left component parts on model 907.633 and must be performed in a similar manner on vehicles with damage on the right side of the vehicle.
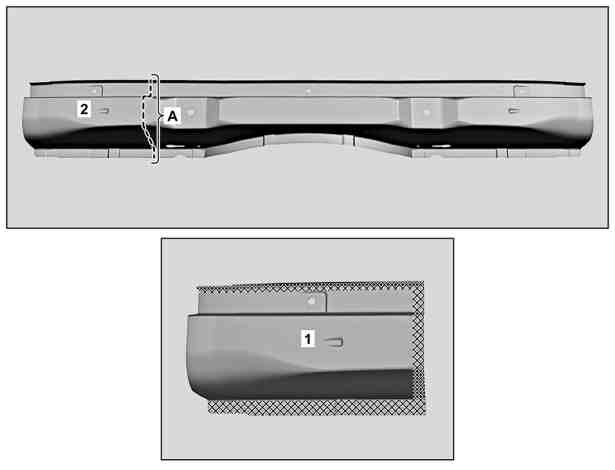
1 | Mark separating point on the new part for the outer part of the rear-end center section (2) (area A). |
Use separating point from vehicle. |
2 | Separate separating point on the new part for the outer part of the rear-end center section (2) (area A). |
Commercially available devices/tools |
3 | Dispose of the larger remaining piece of the new part for the outer part of the rear-end center section (2). |
4 | Grind mating surfaces on rear-end center section (1) down to bare metal in crosshatched areas. |
Sand down spot weld flanges to bare metal on both sides. |
Commercially available devices/tools |
5 | Remove shavings. |
Commercially available devices/tools |
6 | Zinc dust paint to insides of spot weld flanges. |
D64.30-A007-06

7 | Mark separating point on the new part for the inner part of the rear-end center section (4) (area A2). |
Use separating point from vehicle. |
8 | Separate separating point on the new part for the inner part of the rear-end center section (4) (area A2). |
Commercially available devices/tools |
9 | Dispose of the larger remaining piece of the new part for the inner part of the rear-end center section (4). |
10 | Model 907.6/7 |
Commercially available devices/tools |
11 | Model 907.6/7 |
Commercially available devices/tools |
12 | Grind mating surfaces on the inner part of the rear-end center section (3) down to bare metal in crosshatched areas. |
Sand down spot weld flanges to bare metal on both sides. |
Commercially available devices/tools |
13 | Remove shavings. |
Commercially available devices/tools |
14 | Zinc dust paint to insides of spot weld flanges. |
D64.30-A008-06
D64.30-A009-09
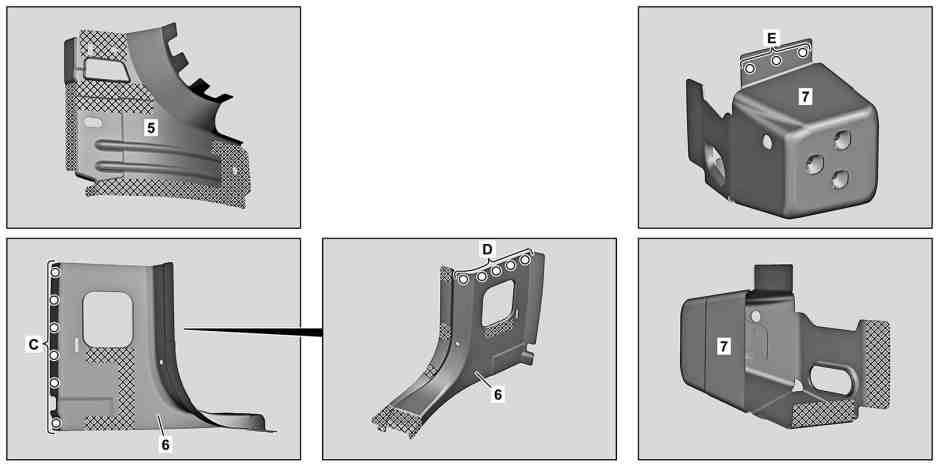
15 | Punch Ø 6 mm holes in the reinforcement (6) (areas C and D) and in the bracket (7) (area E). |
Commercially available devices/tools |
16 | Grind mating surfaces down to bare metal in cross-hatched areas and around holes on the reinforcement (6) (areas C and D) and around holes on the bracket (7) (area E). |
Sand down spot weld flanges to bare metal on both sides. |
Commercially available devices/tools |
17 | Remove shavings. |
Commercially available devices/tools |
18 | Zinc dust paint to insides of spot weld flanges. |