Additional information can be found in the superordinate service document.
The safety information in the superordinate service document must be observed.
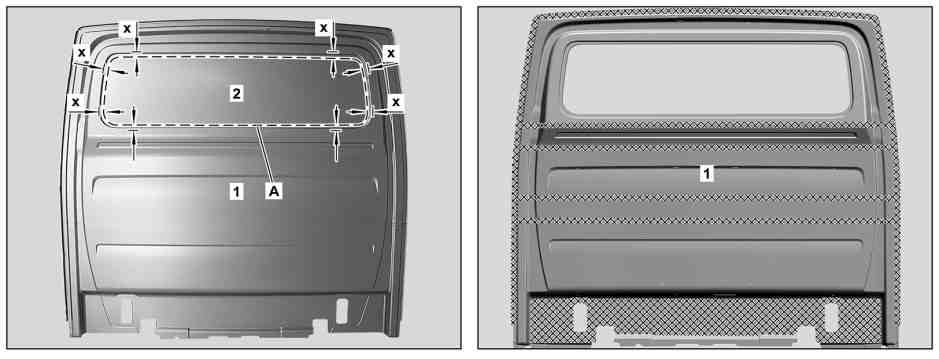
D64.10-1264-08
x | Dimension (13 mm) |
1 | Mark separating point on rear panel (1) as shown (area A). |
Mark separating point next to edge. |
2 | Disconnect rear panel (1) at separating point (area A). |
Commercially available devices/tools |
3 | Remove remaining piece of window cutout (2). |
4 | Grind mating surfaces in cross-hatched areas on rear panel (1) down to bare metal. |
Sand down spot weld flanges to bare metal on both sides. |
Commercially available devices/tools |
5 | Remove shavings. |
Commercially available devices/tools |
6 | Zinc dust paint to insides of spot weld flanges. |
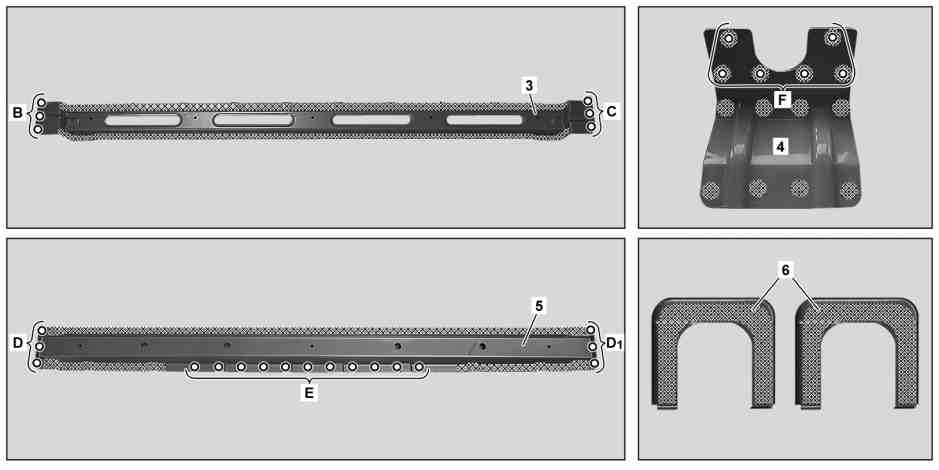
D64.10-1266-09
7 | Punch holes in crossmember (3) (areas B and C), crossmember (5) (areas D, D1, and E), and bracket (4) (area F) with a diameter of 6 mm. |
Commercially available devices/tools |
8 | Grind mating surfaces in cross-hatched areas and around holes (areas B, C, D, D1, E, F) down to bare metal. |
Sand down spot weld flanges to bare metal on both sides. |
Commercially available devices/tools |
9 | Remove shavings. |
Commercially available devices/tools |
10 | Zinc dust paint to insides of spot weld flanges. |

D64.10-1268-07
11 | Grind mating surfaces in cross-hatched areas on reinforcements (7, 8) down to bare metal. |
Sand down spot weld flanges to bare metal on both sides. |
Commercially available devices/tools |
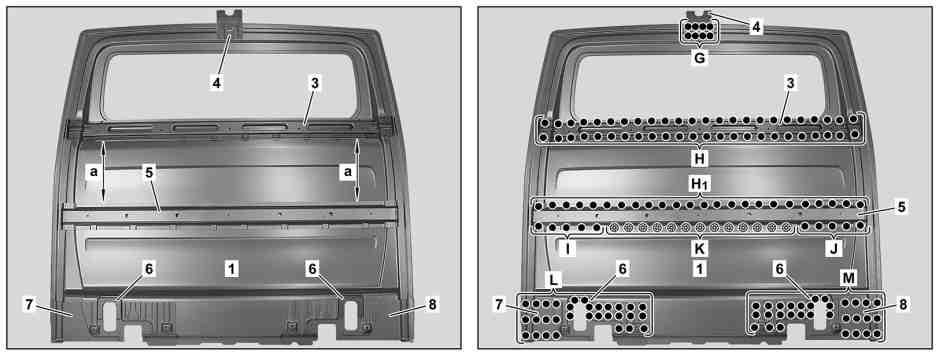
D64.10-1269-08
a | Dimension (325 mm) |
12 | Install reinforcements (6, 7, 8), crossmembers (3, 5), and bracket (4) on rear panel (1), fit, and fix in place. |
Observe dimension (A). |
Commercially available devices/tools |
13 | Reinforcements (6, 7, 8) (areas L and M). |
14 | Bracket (4) (area G). |
15 | Crossmember (3) (area H). |
16 | Crossmember (5) (areas H1, I, and J). |
17 | Crossmember (5) (area K). |
18 | Grind inert gas welds down flat (area K). |
Commercially available devices/tools |
19 | Remove shavings. |
Commercially available devices/tools |

D64.10-1271-09
20 | Punch holes with a diameter of 6 mm in rear panel (1) (areas T, V, W, Y, and Z). |
Commercially available devices/tools |
21 | Grind areas around holes (areas T, V, W, Y, and Z) in rear panel (1) down to bare metal. |
Sand down spot weld flanges to bare metal on both sides. |
Commercially available devices/tools |
22 | Remove shavings. |
Commercially available devices/tools |