33 - 1401 Checking axle parts

Front axle beam
Front axle | A | B | C | D dia. | E | F | G Swivel axis inclination | H |
730. 403 445 | 1440 1 | 56 | 830 | 1) | 56.500 56.310 | 42 | 5° | 32.5 |
730. 404 446 | 64 | |||||||
730. 405 447 448 | 67 | 2) |
Dimension D
Index | 1) | 2) |
Standard | 23.021 ... 23.000 | 26.021 ... 26.000 |
Standard 1 | 23.321 ... 23.300 | 26.321 ... 26.300 |
Repair size 1 | 23.621 ... 23.600 | 26.621 ... 26.600 |
Special tools
Before assembling the front axle check front axle beam visually for cracks and distortion (twisting or bending). Check the dimensional accuracy of the bores for the kingpins and the contact surfaces of the steering knuckle at the stub axles.
If straightening work is necessary, perform only in cold state, otherwise the strength of the tempered material would be lost if heated.
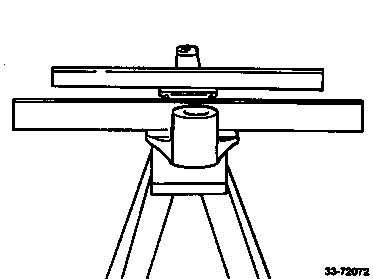
Check front axle beam for twisting
Before straightening ensure that the two spring contact surfaces are parallel. For this purpose place a straightedge with a minimum length of 400 mm on each of the spring contact surfaces and sight across the two straightedges.
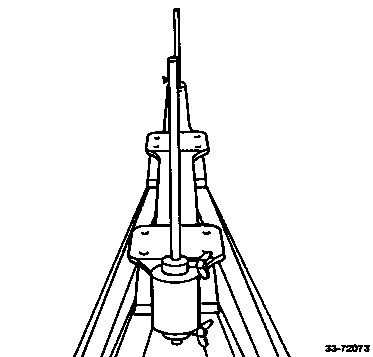
Check stub axles for twisting
Insert special tool in left and right stub axle bore, center and clamp in place with appropriate bushings. Check stub axles for twisting by sighting across the two rods.
Straighten a twisted stub axle only by starting at the clamped spring contact surface.
000 589 01 23 00
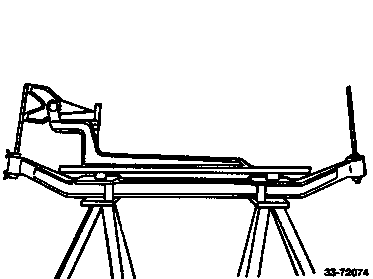
Check stub axle swivel axis inclination
Place straightedge across the two spring contact surfaces and position the adjustable angle gauge. Adjust kingpin inclination so that angle gauge makes contact on left and right sighting rod (observe clearance).
000 589 01 23 00
Straighten front axle beam
Check kingpin bores in stub axle. If the bores are worn, replace front axle beam.
If the contact surfaces on the steering knuckle are worn, refinish with a file or machine set up for this purpose. When refinishing ensure that the top and bottom surfaces are exactly parallel and at right angles to the steering knuckle bore.