AR33.30-W-0535-05B | Mount radial sealing ring and bearing inner race on input shaft | ||
Danger! | Risk of injury to skin and eyes caused by handling hot or glowing objects. | Wear safety gloves, protective clothing and safety glasses, if necessary. |
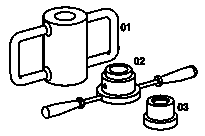
Assembly tool
730 589 05 33 00
Assembly note
To install, heat up the needle bearing inner race to approx. 100 oC.
If possible, heat up the needle bearing inner race in a heating oven. If a heating oven is not available, use a heating plate with sufficient heat output (min. 1500 W).
Monitor the temperature of the needle bearing inner race continuously during the heating phase.
Exceeding the specified temperature can result in material damage which will render the needle bearing inner race unusable.

W33.30-1048-01
1 Clean seat of radial shaft sealing ring and needle bearing inner race as well as axial contact surface on linkage arm and groove (arrow) of O-ring.
2 Clamp drive shaft.
The inner shaft must point upward.
3 Insert new O-ring into groove (arrow) at seat of radial shaft sealing ring.

W33.30-1046-02
4 Push radial shaft sealing ring (2) onto shaft of input shaft.
5 Fit adapter ring (03), drive-in sleeve (02) and impact hammer (01) at input shaft and drive radial shaft sealing ring (2) onto seal ring seat until it touches linkage arm.

W33.30-1049-01
6 Remove grips from drive-in sleeve (02).
7 Insert needle bearing inner race (1) into drive-in sleeve (02) with outer chamfer (arrow) inserted first.
8 Place drive-in sleeve (02) into heating oven with needle bearing inner race (1) pointing upward.
If no heating oven is available, a heating plate can be used instead.
9 Heat up drive-in sleeve (02) with needle bearing inner race (1) to approx. 100 oC.
Monitor the temperature of the needle bearing inner race (1) continuously during the heating phase using a temperature measuring instrument as exceeding the specified temperature can lead to material damage which will render the needle bearing inner race (1) unusable.

W33.30-1047-02
10 Moisten seat of needle bearing inner race (1) on input shaft with oil.
Distribute oil evenly.
11 Push heated needle bearing inner race (1) onto shaft of input shaft using drive-in sleeve (02) and drive onto bearing seat using impact hammer (01) until it touches radial shaft sealing ring.
Insert the handles into the drive-in sleeve (02) to ensure that the needle bearing inner race (1) is guided correctly.
Henviste dokumenter
- as0000z000201a Fare for personskade på hud og øjne ved håndtering af varme eller glødende genstande